Introduction
For OEM engineers, understanding what separates a clinically reliable dental implant from an inferior one starts well before the operating room. It begins with material selection, engineering, manufacturing, and quality assurance.
The global demand for dental implants continues to grow at a projected CAGR of 9.0% from USD 6.0 billion in 2026 to USD 11.0 billion by 2033 (Grand View Research). As their designs become increasingly sophisticated, OEMs require manufacturing partners capable of delivering exceptional precision, repeatability, and regulatory compliance.
Amongst dental implants, titanium dental implants remain the industry standard because of titanium’s unique ability to integrate with bone through osseointegration. It naturally forms a stable titanium oxide (TiO₂) layer that resists corrosion while providing an ideal surface for osteoblast attachment (Titanium Alloy Corrosion Resistant Alloy, Eureka).
This article explores the complete manufacturing process of titanium dental implants: from alloy selection and CAD-driven engineering to precision CNC machining, surface engineering, and quality validation.
How Do You Choose the Right Titanium Alloy for Dental Implants?
Material selection is one of the earliest and most consequential engineering decisions in dental implant manufacturing. The chosen alloy directly influences biocompatibility, fatigue resistance, corrosion behaviour, and long-term clinical performance.
The two alloys used most widely are commercially pure titanium (cpTi / Grade 4) and Ti-6AI-4V (Grade 5). Both have an extensive clinical track record with success rates of up to 99% at 10 years and are biocompatible in contact with bone and gingival tissues (Titanium Alloys for Dental Implants: A Review, MDPI).
Grade 4 CP-Ti
Grade 4 commercially pure titanium contains about 99% pure titanium and no intentional alloying elements.
Controlled oxygen content (up to 0.40%) and iron content (up to 0.50%) provide mechanical strength without compromising biocompatibility. With tensile strength in the 550–680 MPa range, Grade 4 CP-Ti is the standard for most full-diameter implant bodies.
The absence of alloying elements eliminates the risk of ion release into surrounding tissue, making Grade 4 CP-Ti the preferred choice where soft tissue response and allergenic risk matter most.
Grade 5 Ti-6Al-4V
Grade 5 Ti-6Al-4V introduces 6% aluminum and 4% vanadium to reach tensile strengths of 895–900 MPa. This alloy is the material of choice for narrow-diameter implants and angled abutments, where the higher strength-to-diameter ratio is essential.
Trace release of aluminum and vanadium ions remains clinically manageable, and the alloy’s fatigue resistance makes it the right selection for mechanically demanding applications.
Comparison between Grade 4 and Grade 5 Titanium Alloys
The choice between Grade 4 and Grade 5 is application-driven, not a hierarchy of quality. Both are established, clinically validated materials.
| Property | Grade 4 CP-Ti | Grade 5 Ti-6Al-4V | Clinical Implication |
|---|---|---|---|
| Composition | >99% Titanium | 90% Ti, 6% Al, 4% V | No alloying element release |
| Tensile Strength | 550–680 MPa | 895–900 MPa | Higher strength for narrow implants |
| Biocompatibility | Excellent | Excellent (trace ion release) | Grade 4 preferred for allergy-sensitive patients |
| Corrosion Resistance | Superior | Excellent | Both suitable for long-term implantation |
| Primary Use | Standard implant bodies | Narrow implants, angled abutments | Application-driven selection |
Beyond material properties, Grade 4 CP-Ti carries two clinical advantages that matter at the point of care:
- Its non-ferromagnetic nature makes titanium dental implants fully compatible with MRI procedures, simplifying post-operative patient management,
- The absence of alloying elements presents essentially zero allergenic risk – an increasingly important consideration as metal sensitivity awareness grows and patient screening becomes more rigorous.
Zirconia
Zirconia (all-ceramic) implants occupy a smaller but growing niche, primarily for patients with confirmed titanium sensitivity.
Their all-ceramic composition offers aesthetic advantages in thin tissue biotypes, but titanium remains the dominant material for the vast majority of clinical indications.
For a broader view of material selection criteria across device categories, refer to Acrotec Medtech’s article Choosing the Right Materials for Your Medical Device.
How Are Titanium Dental Implants Engineered and CNC Machined?
Before a titanium stock enters a CNC (Computer Numerical Control) machine, the implant geometry is fully defined in CAD (Computer-Aided Design).
CAD and Prototyping
Advanced 3D CAD software allows engineers to simulate the exact shape, thread geometry, taper, and internal connection of the implant body with micron-level precision.
This digital-first approach reduces human error and supports multiple design iterations before any material is committed.
Modern dental implant designs -measured in microns- incorporate several geometry-critical features:
- Thread profiles optimized for primary stability across varying bone densities,
- Tapered or cylindrical body geometries matched to specific drilling protocols,
- Internal hexagonal or conical connection interfaces for abutment coupling,
- Macro- and micro-scale surface features designed to promote cell adhesion.
Once the implant geometry has been validated digitally, the next step is prototype evaluation. Rapid prototyping -using 3D printing- enables OEMs to verify fit, functionality, and manufacturability before committing to production tooling, reducing development risk while accelerating design iterations.
The validated CAD model then becomes the blueprint for CNC manufacturing.
CNC Machining
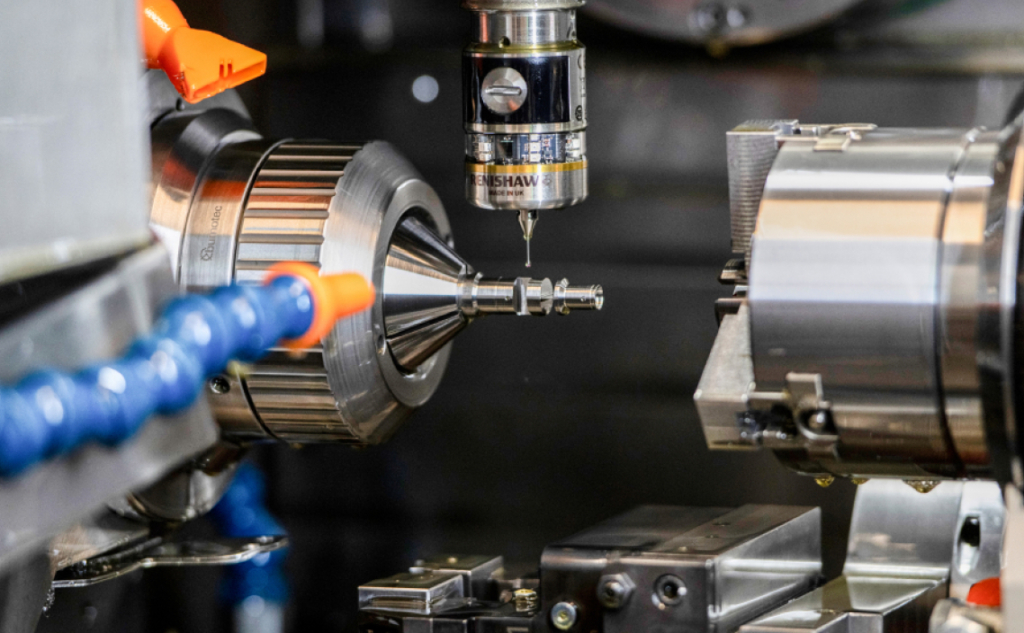
The transition from digital design to a finished implant takes place through multi-axis CNC turning and milling.
Unlike conventional machining, dental implant manufacturing operates at micron-level tolerances, where even minimal dimensional deviations can affect implant performance.
Three manufacturing capabilities are particularly critical:
- Dimensional accuracy: thread geometry, implant diameter, and internal connection interfaces must precisely match the design specification. Deviations of only a few microns can compromise prosthetic fit and sealing performance,
- Repeatability: every implant in a production batch must be virtually identical. High-end CNC systems deliver this consistency at production scale,
- Material integrity: titanium is challenging to machine because of its low thermal conductivity and tendency to generate heat. Optimised tooling, cutting parameters and coolant management preserve its microstructure while preventing burr formation, thermal damage and premature tool wear.
For further information on the impact of deviations, consult our article on how tight tolerances affect medical device performance (link to be inserted).
In addition to CNC machining, Selective Laser Melting (SLM) is gaining ground as a complementary technique, particularly for porous scaffold structures that mimic cancellous bone architecture. Interconnected porosity produced by SLM reduces stress shielding compared to fully solid machined surfaces. It is relevant for specific implant body designs targeting enhanced bone ingrowth.
How Do Surface Engineering Techniques Improve Osseointegration?
A precision-machined implant may meet every dimensional specification, yet still fall short biologically. Surface engineering transforms it into one that promotes rapid osseointegration, accelerates healing, and supports long-term clinical success.
A number of surface treatments are available for titanium dental implants, and the choice depends on the clinical performance targets defined for a specific implant line.
Some are applied in isolation; others are combined to achieve hierarchical surface topographies. This section covers the four most clinically established and commercially proven methods: SLA (Sandblasting and Acid Etching), Anodic Oxidation, Laser Micro-Texturing, and Plasma Spraying.
SLA: Sandblasting and Acid Etching
SLA combines two sequential processes:
- Sandblasting: aluminum oxide or titanium dioxide particles blast the surface to create macro-scale roughness, increasing surface area and promoting mechanical interlocking with bone,
- Acid Etching: an acid etch – using sulfuric acid, hydrochloric acid, or a combination – creates micro-pits at the 1–3 µm scale.
The result is a hierarchical surface topography that expands bone contact area and promotes protein adsorption.
SLA surfaces are among the most clinically documented and remain a benchmark against which newer surface technologies are measured.
Anodic Oxidation
Anodic oxidation uses electrochemical processing to grow a thicker, more bioactive TiO₂ layer enriched with calcium and phosphorus ions. The resulting surface accelerates bone mineralization and enhances the early biological response of surrounding tissues, shortening the osseointegration timeline in certain clinical protocols.
Laser Micro-Texturing
Laser micro-texturing uses focused laser energy to produce controlled micro- and nano-scale patterns on the titanium surface with high reproducibility. Beyond osseointegration benefits, laser-textured surfaces demonstrate reduced bacterial adhesion compared to acid-etched surfaces – which directly addresses peri-implant infection risk, a leading cause of late implant failure.
Plasma Spraying
Plasma spraying applies molten bioactive materials – typically hydroxyapatite – onto the implant surface at high velocity. It creates a rough, chemically active coating that promotes rapid bone bonding. The plasma-sprayed layer provides both mechanical interlocking and chemical affinity for bone tissue.
Coating adhesion and long-term stability require rigorous process control, but when properly executed, plasma-sprayed surfaces deliver strong early fixation and accelerated healing timelines.
How Is Quality Control Ensured for Titanium Dental Implants?
Before release, every implant undergoes rigorous inspection to verify dimensional accuracy, surface quality, mechanical integrity, and regulatory compliance.
Quality control for dental implants covers four main areas:
- Dimensional verification: Coordinate Measuring Machines (CMMs) and optical profilometers confirm that thread geometry, diameter, length, and connection interface all fall within specification,
- Surface characterization: profilometry quantifies surface roughness parameters (Ra, Sa) to confirm that surface treatment outcomes meet specification consistently across production batches,
- Mechanical testing: implants undergo fatigue testing that simulates years of cyclic masticatory load to verify long-term structural integrity,
- Biocompatibility validation: material and surface testing against ISO 10993 standards confirms cytotoxicity, sensitization, and systemic toxicity compliance before any clinical release.
After passing inspection, implants are packaged in sterile barrier systems within ISO-classified cleanroom environments.
Each unit carries full traceability data:
- Batch number,
- Material heat number,
- Surface treatment lot, and
- Expiration date.
This traceability infrastructure supports post-market surveillance and allows manufacturers to respond rapidly to any field quality event.
Conclusion
Titanium has remained the benchmark material for dental implants for decades, but the technology continues to evolve.
Advances in additive manufacturing, surface engineering, digital workflows, and patient-specific implant designs are pushing the boundaries of implant performance and manufacturing precision.
As these innovations accelerate, the challenge for OEMs will not simply be selecting the right material, but partnering with manufacturers capable of delivering increasingly complex designs with consistent quality and regulatory compliance.
This is where experienced contract manufacturing partners play a critical role.
Acrotec Medtech combines advanced precision machining, specialised surface engineering, and rigorous quality systems to help OEMs bring high-performance dental implant solutions to market with confidence.
If you are developing or scaling a dental implant line and need a contract manufacturing partner with proven expertise in titanium machining, surface treatment, and ISO 13485-certified production, contact Acrotec Medtech to discuss your requirements.